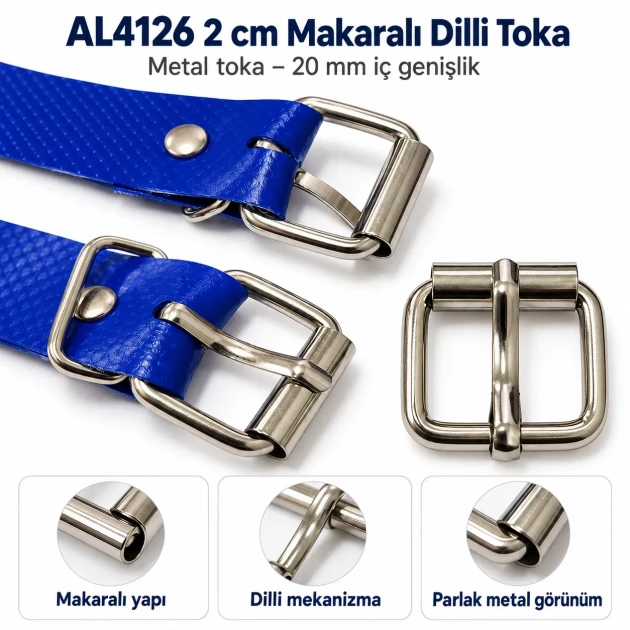
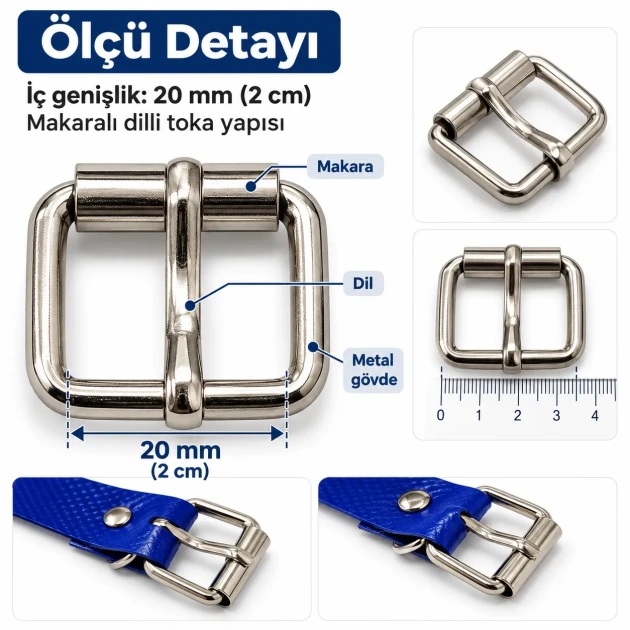
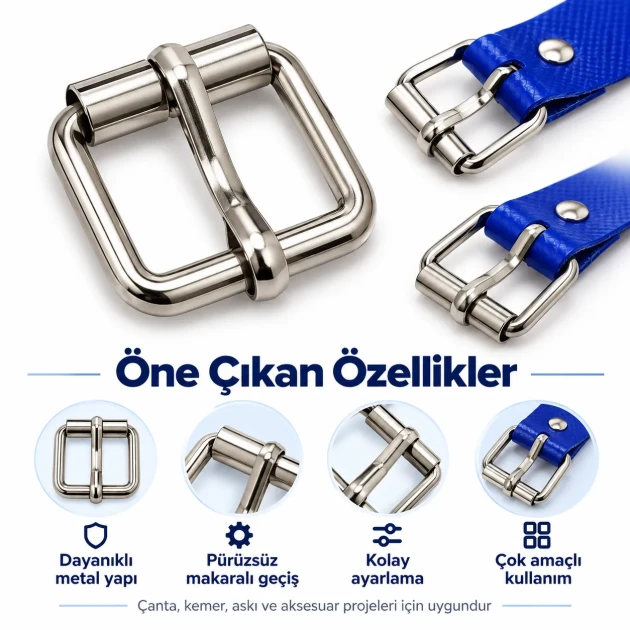
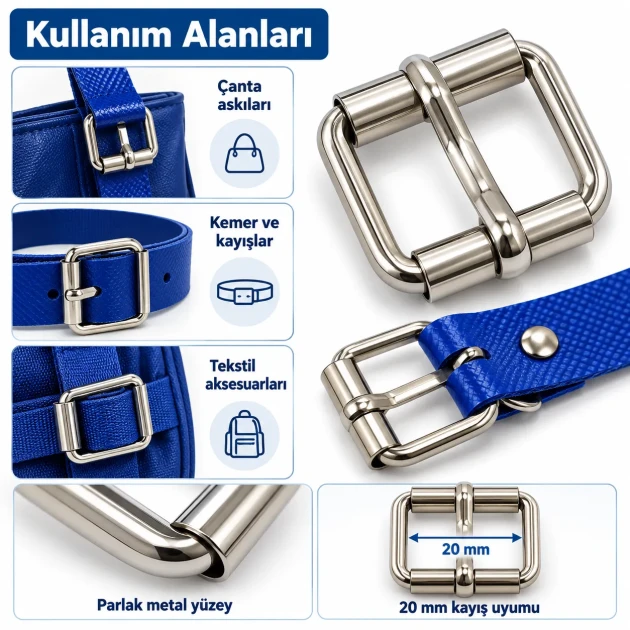
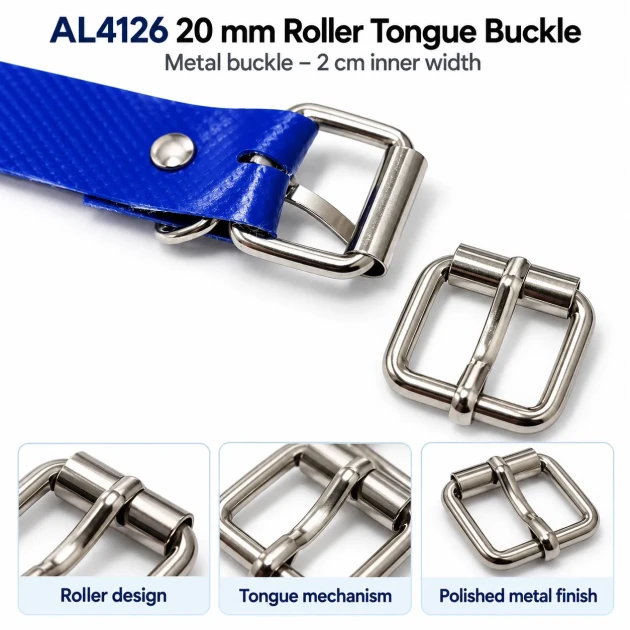
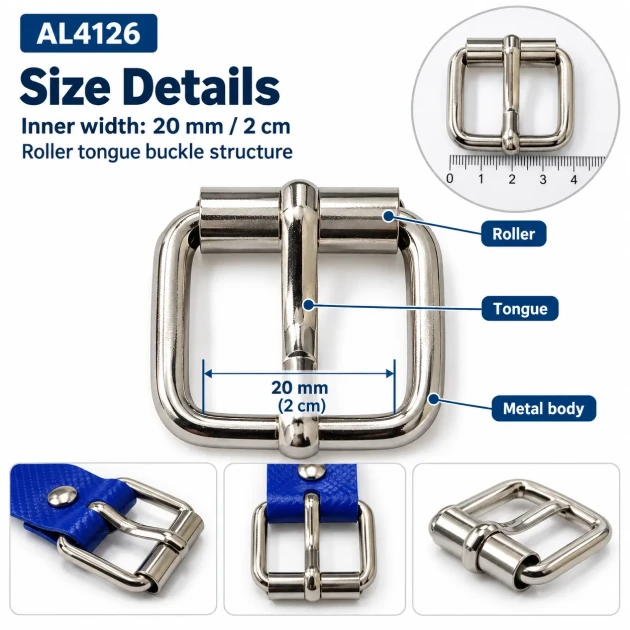
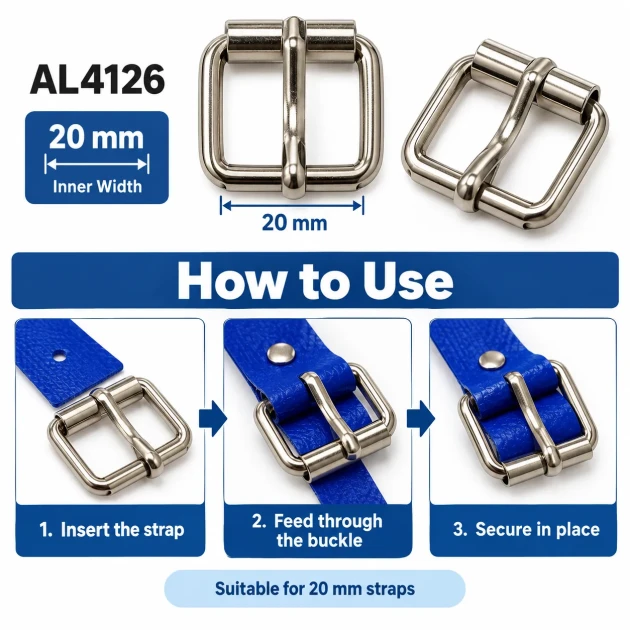
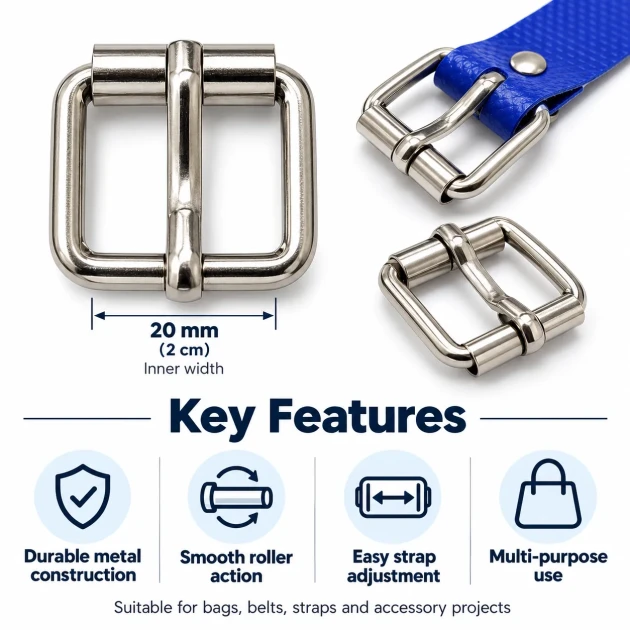
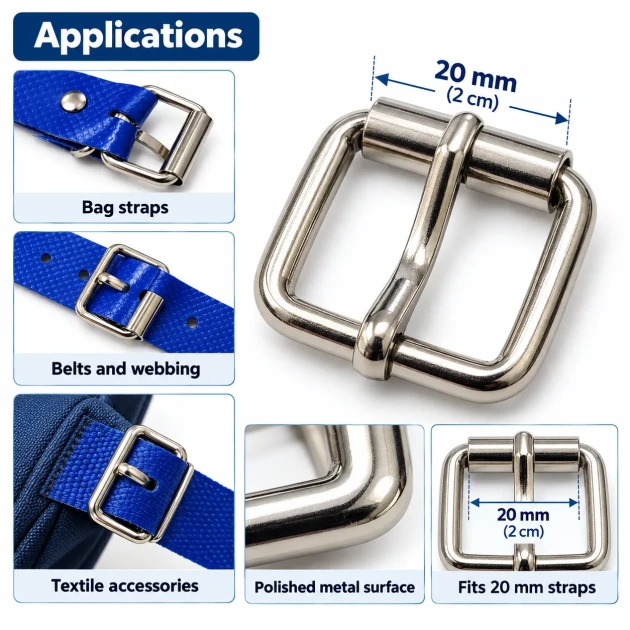
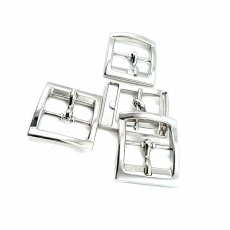
AL4126 is a 20 mm / 0.79 in roller pin buckle intended for strap constructions that use a fixed hole-and-pin adjustment system. The supplied manufacturer catalog image identifies item 4126 and lists the dimensional sequence as 3.90 × 20 × 14 mm. The image does not label which axis each number represents, so this product page intentionally preserves the sequence instead of inventing terms such as wire diameter, inside height, or outside width. For buying and production decisions, treat 20 mm / 0.79 in as the nominal strap class, then confirm the actual finished strap with a physical sample.
Why This Buckle Is Different From a Basic Frame Buckle
A roller pin buckle is more than an open metal frame. It combines a pin, which enters a prepared hole in the strap, with a roller positioned along the edge where the strap changes direction. The roller can rotate as the strap moves around that side of the buckle. That does not make the hardware a slider buckle and it does not guarantee reduced wear in every material, but it changes the way the strap contacts the frame.
This construction is useful when a designer wants a traditional buckle closure with visible adjustment holes while also using a roller at the strap turn. The correct application depends on the full assembly: finished strap width, thickness, fold, hole layout, attachment method, and expected use. A buckle should never be selected from the nominal width alone.
Start With the Finished Strap, Not the Raw Cut Width
A common sourcing mistake is measuring a strip before sewing or finishing and then ordering hardware based only on that number. A raw 20 mm strip can become slightly wider or narrower after edge folding, edge paint, lamination, reinforcement, skiving, backing, or stitching. Thickness can change even more dramatically at the folded buckle end.
For AL4126, measure the exact section that will work inside the buckle after every production step is complete. If your free strap end is one layer but your fixed buckle end is two or three layers, record both conditions. This makes it easier to identify whether a fit problem comes from width, thickness, or fold geometry instead of blaming the buckle without testing the assembly.
How to Use the 3.90 × 20 × 14 mm Catalog Reference
The manufacturer catalog provides three numbers: 3.90, 20, and 14 mm. Because the source does not identify the measurement axes, the responsible way to use the information is as a reference sequence rather than a complete engineering drawing. The 20 mm figure is consistent with the 2 cm commercial strap category, but the other two values should not be assigned an unsupported meaning.
If your production needs exact clearances, use calipers on a physical sample. Measure the points that matter to your own pattern: the available strap path, frame spacing, pin reach, roller location, or folded-end clearance. Then place those measured values into your internal tech pack. This separates verified factory-catalog information from measurements taken specifically for your own project.
20 mm / 0.79 in Is a Nominal Hardware Class
In U.S. buying language, 20 mm equals approximately 0.79 in. That conversion helps teams working with inch-based patterns, but the metric measurement should remain the primary technical reference because the source catalog is metric. Do not round 20 mm to a full 1 in when planning the strap. A 1 in strap is about 25.4 mm and belongs to a different size range.
Use 0.79 in only as an inch equivalent for recognition. When making dies, patterns, or cut files, work from the real metric dimension and the tested sample. This is particularly important if multiple factories or suppliers use different sizing conventions.
Leather Belt Applications
For a leather belt, AL4126 can be evaluated when the finished strap is in the 20 mm class. The fixed buckle end is normally folded back and secured, which can double the leather thickness before adding lining, adhesive, stitching, or a fastener. A strap that moves easily through the buckle as a single layer may still become bulky at the fold.
Build the complete buckle end before approving the hardware. Make sure the pin can move freely, the roller is not blocked by the folded leather, and the stitch line does not make the fold unnecessarily rigid. Then create one test hole and close the buckle several times. Watch for excessive stretching, tearing, or misalignment at the hole.
Bag Closure and Leather Tab Applications
On a bag, a roller pin buckle may be used on a flap strap, closure tab, decorative leather strap, small case, pouch, or organizer. The mechanical demand can be different from a waist belt. Some bag closures are opened dozens of times per day, while others are mainly decorative and carry little tension.
Define the user interaction before selecting the hardware. If the customer needs fast continuous adjustment, a slider may be a better solution. If the design calls for a classic pin-and-hole closure, AL4126 belongs to the correct hardware family. Strap length, hole count, and free-end management should all be planned around the intended use.
Webbing and Textile Strap Applications
Woven webbing can maintain width more consistently than natural leather, but the fixed end can become thick when folded. Stitching, reinforcement tape, folded edge treatments, and multiple layers all affect the local stack. A roller buckle should be tested with the full fold, not with a single loose strip.
Prepare a short production-style sample using the actual webbing and stitch pattern. Fold the end, attach it the way production will attach it, and operate the buckle. Confirm that the roller still moves, the pin is accessible, and the frame does not distort the webbing. If the stack is too thick, changing the fold construction may solve the issue without changing the nominal strap width.
Faux Leather and Laminated Strap Applications
Faux leather can include a top coating, textile backing, foam, reinforcement, or lining. These layers may behave differently under a pin hole than natural leather. The material can also become significantly thicker when folded around the buckle end. Because of those variables, the nominal 20 mm width is only one part of compatibility.
Test the hole on the actual finished material. Check whether the backing stretches, the surface cracks, or the hole enlarges after repeated fastening. No verified hole diameter or punching-die specification is available for AL4126, so the production hole should be developed around the actual pin and material combination.
Pin Hole Development
A pin buckle depends on a properly planned hole. The hole must admit the pin without excessive force, yet it should not be so large that the strap sits loosely at the selected adjustment point. Hole geometry may be round, oval, or slot-like depending on the strap and pin shape. The supplied catalog image does not provide a validated hole specification.
Start with one test hole. Fasten and unfasten the buckle several times under realistic hand tension. Inspect the material around the hole. If the edge deforms quickly, revise the hole size, reinforcement, or material preparation. Only after the test succeeds should the full hole pattern be added to the production template.
Hole Spacing and Adjustment Range
Hole spacing is part of product ergonomics. On a belt, holes that are too far apart can make it difficult to achieve a comfortable fit. On a bag closure, only a small amount of adjustment may be needed. There is no verified AL4126-specific hole-spacing standard, so spacing should be determined by the finished product design.
When possible, identify the central or most common adjustment position first, then build the surrounding hole pattern from that point. This helps balance the visual layout and the functional range. Always test the shortest and longest intended positions, not just the center hole.
Roller Pin Buckle vs. Center-Bar Pin Buckle
These hardware types can look similar in a catalog but should not automatically be treated as substitutes. A center-bar buckle uses a central bridge as an important structural and attachment feature. A roller buckle emphasizes the rotating element at the strap turn. Differences in frame geometry, pin placement, and fixed-end attachment can require different strap patterns.
If you are replacing an existing buckle, compare the old part and AL4126 side by side. Check pin length, roller position, attachment clearance, and how the strap folds around the frame. A shared nominal width does not guarantee drop-in compatibility.
Roller Pin Buckle vs. Slider Buckle
A slider buckle usually provides continuous adjustment by routing the strap through one or more bars. A roller pin buckle provides fixed adjustment points through holes or slots. These systems create different user experiences. Choosing one in place of the other can change how the product is worn, opened, or adjusted.
Before purchasing, ask whether your design needs discrete adjustment points or continuous length control. If discrete holes are part of the design language, AL4126 is in the appropriate category. If the strap must move freely without holes, evaluate a slider-style component instead.
Attaching the Fixed Strap End
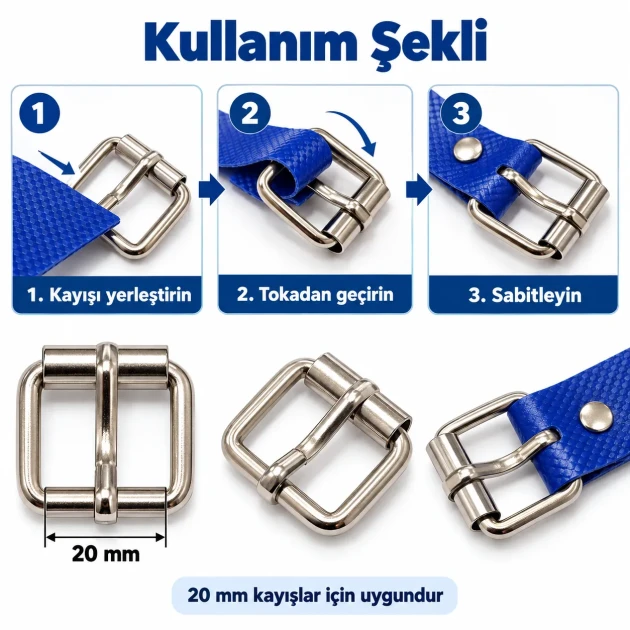
This buckle is not installed like a snap, eyelet, or rivet that is pressed directly into fabric. One end of the strap must be secured around the buckle structure. Depending on the product, the fixed end may be folded and stitched, secured with a suitable rivet or screw, or attached by another method chosen by the designer.
No specific rivet, screw, or attachment hardware has been verified as included with AL4126. Plan those components separately. If using a rivet, choose a post length appropriate for the full material stack. If stitching, place the seam so the fold remains flexible enough for the buckle to work normally.
Why Alloy Type Is Listed as Unspecified
The supplied image supports describing the component as metal, but it does not verify a specific alloy. This page therefore avoids claiming zinc alloy, brass, steel, stainless steel, or another composition without evidence. That distinction is important for projects with weight, corrosion, plating, magnetic, restricted-substance, or compliance requirements.
If composition matters to your product, request technical confirmation before production. Do not use appearance alone to infer the alloy. A plated surface can make different base metals look similar.
Finish and Color Planning
No verified finish list has been provided for AL4126 yet. Similar hardware may exist in nickel, black nickel, gold, antique brass, gunmetal, or other finishes, but those colors should not be promised for this item until the actual options are confirmed. Product photography and option data should be used to finalize the finish information later.
For collections that use several metal components, compare the buckle with rings, snaps, rivets, zipper sliders, or chain under the same lighting. Matching only by finish name can be misleading because tone and gloss vary between suppliers and production lots.
Prototype Procedure for Product Developers
Use the actual production material and make a complete buckle-end sample. Add the real lining, reinforcement, edge finish, stitch, rivet, or screw. Install the buckle and form one test hole. Operate the closure repeatedly while watching the pin, roller, fold, and hole.
Then evaluate appearance. Does the strap sit centered in the frame? Is the buckle square to the strap? Does the folded end create an unwanted lump? Does the free end align with the keeper or next hardware component? A functional fit that looks visually uneven may still require a pattern adjustment.
Incoming Inspection for Production Orders
When hardware arrives, a basic incoming check can review the model identity, visible shape, roller movement, pin alignment, obvious burrs, distortion, and surface appearance. These are general quality-control suggestions, not a published manufacturer inspection plan for AL4126.
Compare representative pieces with the approved sample. If there are multiple cartons or lots, sample from more than one package. Record delivery or lot information so any later assembly issue can be traced back to the hardware batch.
On-Line Assembly Checks
After attachment, verify that the folded strap end is secure and does not interfere with the pin. Close the buckle at one or more planned adjustment holes. The strap should lie naturally rather than twisting sharply to one side. The roller should not be locked by stitching, a rivet head, or excess material.
If the same buckle is used with several strap materials, inspect each construction separately. A leather version and a webbing version may have the same width but very different folded thicknesses.
Dimensional Tolerance in Real Production
Nominal 20 mm does not mean every finished strap will measure exactly 20.00 mm. Cutting, coating, folding, and sewing can introduce variation. Product developers should define an acceptable finished range based on the approved sample. That range can then become part of incoming material and in-process quality control.
If a later material lot begins to bind in the buckle, measure the strap before assuming the hardware has changed. Likewise, if a new hardware lot feels different, compare both the buckle and the strap to the approved references. Controlled measurement prevents unnecessary component changes.
Cost of a Hardware Mismatch
A buckle is a small component, but the wrong choice can create expensive rework. A strap may need to be recut, skived, re-stitched, re-punched, or re-patterned. A hole die may need to change. A closure may need to be redesigned. These downstream effects often cost more than the difference between two buckle prices.
The practical way to control that risk is to approve the hardware and strap together before releasing the production pattern. Keep the approved sample and write the buckle code into the tech pack so purchasing does not substitute a different 20 mm model without review.
What to Record in a Tech Pack
A useful tech-pack entry can include: product code AL4126; hardware type roller pin buckle; nominal strap class 20 mm / 0.79 in; manufacturer catalog dimensions 3.90 × 20 × 14 mm; material description “metal, alloy unspecified”; approved finish; finished strap width; finished strap thickness; buckle-end fold length; attachment method; hole dimensions; hole spacing; and sample approval date.
Photos of the approved assembly are also useful. One front view, one back view, and one side view can show details that are difficult to communicate with numbers alone. If a finish is important, retain a physical master sample as well.
How to Compare Other 20 mm Buckles
When comparing hardware in the same nominal size, first compare function. Is it a roller pin buckle, center-bar buckle, fixed frame, slider, or another system? Second, compare the actual geometry. Third, compare material and finish requirements. Fourth, test the candidate on the same finished strap.
This sequence prevents a common sourcing error: selecting a visually similar component that belongs to a different functional family. A 20 mm label is a starting point, not the complete specification.
Storage and Handling
No specific chemical or plating durability data has been verified for this model. Avoid assuming resistance to salt water, detergents, solvents, machine washing, or outdoor exposure. If the final product will encounter those conditions, test the complete assembly and finish before approving care instructions.
During storage, metal pieces can rub against one another and develop cosmetic marks. If appearance is critical, use appropriate separation or packaging and define what level of surface variation is acceptable before final assembly.
When a Physical Sample Is Essential
A physical sample is essential when the pattern has tight clearances, when the strap is thick or heavily layered, when a custom hole die will be ordered, when the finish must match other hardware, or when the product will be made in large quantities. The sample should also be used whenever the application depends on a specific pin angle, fold location, or visual alignment.
Do not treat a catalog photo as an engineering drawing. The image can identify the product and general construction, but the final manufacturing decisions should be based on the real part.
Product Photography Check Before Activation
This listing is intentionally being prepared before final product images are uploaded. Once the actual gallery is added, re-check the visible finish, roller shape, frame proportions, and any details that can be confirmed from the new photographs. If the images reveal verified information not present in the catalog source, update the attributes accordingly.
The image ALT and TITLE text should then be matched to the real photographs rather than using generic phrases. Technical images should show only verified measurements and avoid invented material or finish claims.
Quick Buyer Decision Flow
Step one: confirm that the project needs a pin-and-hole closure. Step two: confirm that the finished strap is in the 20 mm / 0.79 in class. Step three: build the actual folded buckle end. Step four: test one hole. Step five: check roller movement and alignment. Step six: document the approved setup before ordering or producing at scale.
If one of these steps fails, identify the reason before increasing order quantity. The problem may be the strap construction, hole layout, attachment method, or the fact that another buckle family would suit the product better.
Frequently Asked Questions
What strap size is AL4126 intended for?
It is intended to be evaluated in the 20 mm / 0.79 in strap class. Finished strap width and thickness should be confirmed with a physical sample.
What dimensions are verified?
The manufacturer catalog image lists 3.90 × 20 × 14 mm. Because the source does not label the axes, the sequence is preserved exactly.
Is this a roller buckle?
Yes. It combines a roller at the strap-turn edge with a pin for hole-based adjustment.
Can it be used on leather belts?
It can be evaluated for 20 mm-class leather belts. Test the finished fold, thickness, pin movement, and hole geometry before production.
Can it be used on bag straps?
It can be used in suitable bag closure or accessory strap designs where a pin-and-hole fastening system is appropriate.
Does it work like a slider buckle?
No. A pin buckle uses fixed holes or slots. A slider normally provides continuous adjustment through strap routing.
Is a press required?
The buckle itself is not press-set into fabric. The fixed strap end is attached using the method selected for the product, such as stitching or suitable fastening hardware.
Are rivets included?
No included rivet, screw, or other attachment component has been verified for this item.
Is the alloy zinc?
The alloy type is not verified. The component is described as metal without naming a specific alloy.
Which finishes are available?
A verified AL4126 finish list is not yet available. Finish information should be updated after actual product options and images are confirmed.
How do I know my strap will fit?
Measure the completed strap, build the real folded buckle end, create one test hole, and approve the full assembly with the physical buckle.
Can this be used in safety equipment?
No verified load rating or safety certification is available for AL4126. Safety-critical uses require separate engineering testing and approval.
Final e-Buttons Selection Guidance
AL4126 should be purchased as a specific roller pin buckle model, not as a generic “20 mm buckle.” The nominal size helps narrow the search, while the real sample confirms the production fit. Keep the manufacturer catalog measurement sequence with your sourcing records, but use your own verified sample dimensions for pattern and tooling decisions.
For repeat production, the most reliable standard is an approved physical sample supported by a written tech pack. That combination gives design, sourcing, production, and quality teams the same reference and reduces the risk of an unreviewed hardware substitution later.